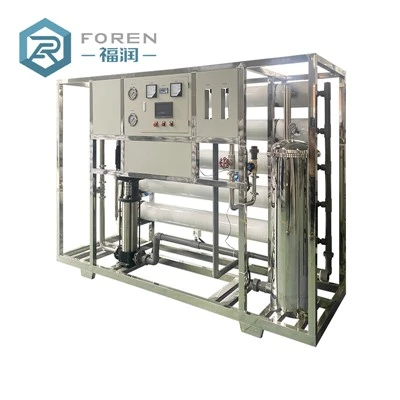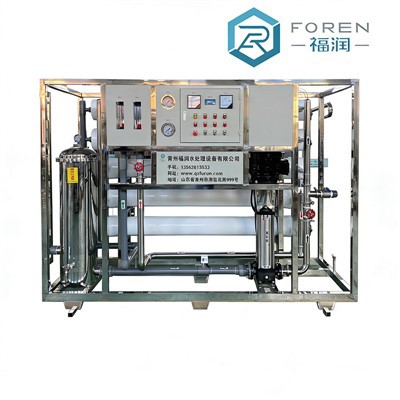


Industrial reverse osmosis system blocks up to 99% bacteria, particles, sugars, proteins, dyes and impurities (molecular weight > 150-250 Daltons) in water, thereby products pure water.
Qingzhou Foren Water Treatment Equipment Co., Ltd. customizes industrial reverse osmosis system of various specifications. With water treatment capacity ranging from 500 L/h to 400000 L/h, we meet diverse industrial water treatment needs.
FOREN's reverse osmosis system offer configuration options, such as: motor brand, overall machine material, machine size, control system, etc. This ensures operation of the water treatment system under various environmental conditions.

Compact Industrial Reverse Osmosis Equipment:
Equipped with media filter and chemical dosing system (pre-chlorination, scale inhibitor, dechlorination, post-chlorination, post-pH adjustment).
Containerized RO Water Treatment Plant:
Ideal for outdoor use with no size restrictions. Equipped with a container shell for convenient outdoor placement.

Industrial RO system flow chart:
The industrial RO system is composed of key components working together to deliver purified water.
Pretreatment Stage: Removes large particles, sediments and organics via filtration, sedimentation and activated carbon adsorption, protecting RO membranes from fouling and damage.
Pressurization Stage: High-pressure pump pushes pretreated water through semipermeable RO membranes, which only allow pure water molecules to pass while retaining dissolved solids and contaminants.
After the entire reverse osmosis water treatment system, purified water (permeate) is collected for use, and concentrated wastewater (brine) is discharged. The brine energy is be recycled with energy recovery devices to enhance efficiency.

To ensure optimal performance and service life of the industrial RO system, please note the following:
1. System Design: Rational design (accurate sizing, proper membrane selection and operation condition consideration) is key to expected results. Cooperate with experienced professionals and reputable water treatment equipment manufacturer for efficient, reliable design.
2. Pretreatment: Effective pretreatment protects RO membranes from fouling, scaling and premature damage. Custom pre-filtration, pH adjustment and chemical dosing (based on feed water characteristics) are essential for optimal performance.
3. Monitoring & Maintenance: Regularly monitor pressure, flow rate and water quality to detect deviations or issues promptly.

Hot Tags: industrial reverse osmosis system, China industrial reverse osmosis system manufacturers, suppliers, factory, Single Stage Reverse Osmosis System, Double Pass Reverse Osmosis System, reverse osmosis system, industrial reverse osmosis water system, Single Stage RO System, commercial ro system