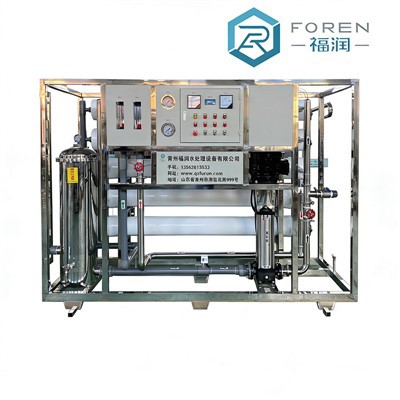


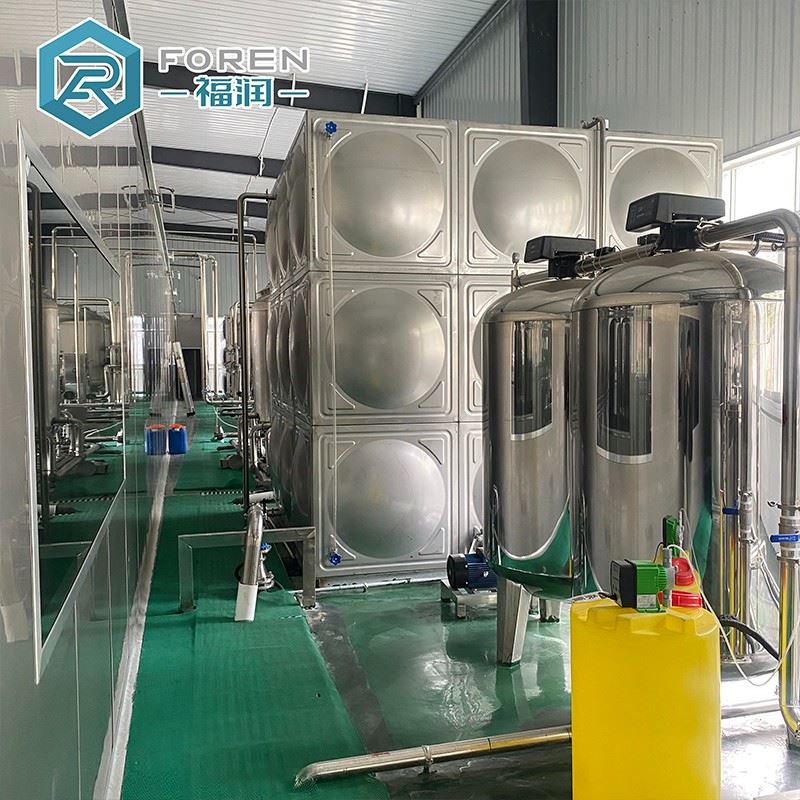

After years of on-site research and project iteration for drinking water factories, Qingzhou Foren Water Treatment Equipment Co., Ltd. has independently developed and launched this 30-ton per hour large scale reverse osmosis system. We designed this equipment specifically to solve the core pain points of medium and large-sized water plants, including unstable water quality, insufficient continuous water supply, and high equipment failure rates in bottled and barreled water production.
Different from ordinary small RO water purification devices, this full-set industrial water treatment equipment is a complete integrated production line tailored for commercial drinking water production. It can directly convert raw water such as underground water and tap water into standard purified water that fully meets the production requirements of bottled pure water, barreled drinking water and daily beverage water. In actual factory operation scenarios, this equipment can support 24-hour continuous stable water output, perfectly matching the high-frequency and large-volume production rhythm of professional water plants.
The large scale reverse osmosis system covers all links from raw water pretreatment, core reverse osmosis purification, real-time water quality monitoring to terminal disinfection and finished water storage. It can effectively filter and remove suspended sediments, residual heavy metal ions, soluble salts, bacteria and microbial impurities in raw water. The final water quality is stable and compliant, which can directly serve the subsequent filling and packaging processes of bottled and barreled water.

Real Equipment Structure & On-site Operating Advantages
We have optimized every structural module of the equipment based on the actual operation feedback of hundreds of water plant projects, abandoning overly complicated redundant designs and focusing on practicality, stability and low maintenance cost for industrial production.


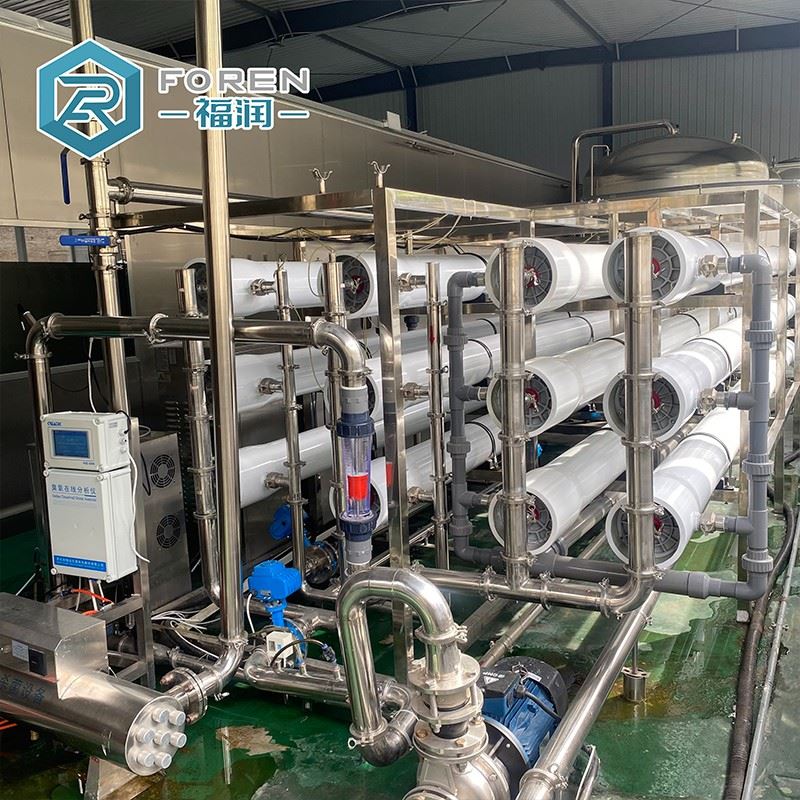
The front-end pretreatment system is the key to prolonging the service life of the core equipment. We adopt food-grade 304 stainless steel water tanks and multi-stage filter devices including multi-media filters and activated carbon filters. In actual use, this configuration can effectively intercept sediment, impurities and residual chlorine in raw water, and match the automatic softening and dosing scale inhibition system. This avoids membrane scaling and damage caused by long-term high-load operation, which is a common failure of many low-cost water treatment equipment on the market. All pipelines and containers comply with food-grade hygiene standards, with no secondary pollution to water quality.
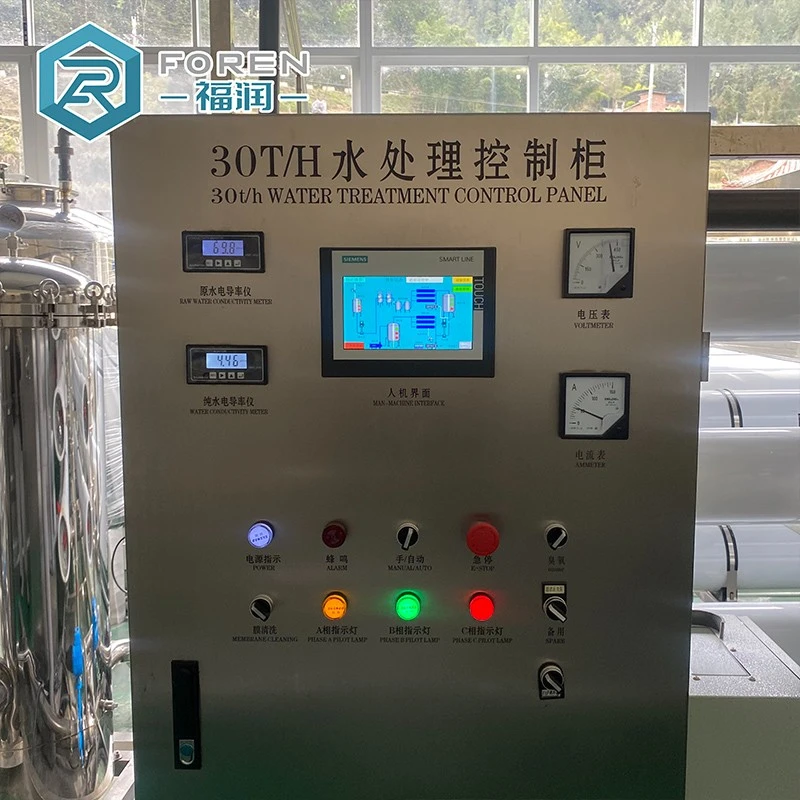
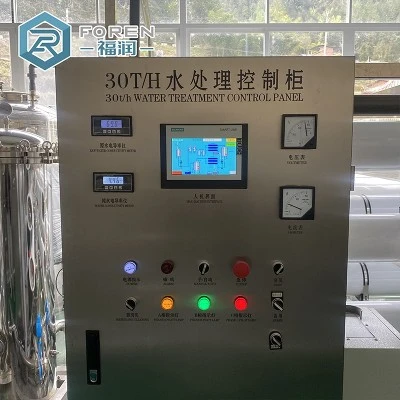
The core 30T/H reverse osmosis main unit is the core guarantee of water yield and water quality. We equip the system with high-efficiency industrial RO membrane elements and high-pressure booster pumps selected through practical tests. Compared with ordinary membrane elements, our matched accessories have higher salt rejection rate and more stable filtration performance. The whole system adopts intelligent PLC touch screen automatic control, which is very friendly for factory operators. Workers can intuitively check real-time data such as water conductivity, operating pressure and water flow on the screen, and support manual and automatic switching operation. Most importantly, the equipment supports unattended continuous operation, which greatly saves the labor cost of factory daily production.
In view of the hygiene requirements of drinking water production, we have added a terminal UV sterilization unit and a sealed sanitary finished water tank. After RO deep purification, the water will be sterilized again to eliminate residual microorganisms, and the sealed storage design completely avoids secondary pollution caused by open placement. All pipe connections adopt sanitary quick-install joints, which is convenient for daily CIP cleaning and regular equipment maintenance, effectively reducing the downtime maintenance rate of the production line.
In actual factory application, this 30-ton large scale reverse osmosis system has obvious advantages: stable hourly water output meets the daily large-scale production demand of medium and large water plants; the overall energy consumption is optimized and reduced compared with traditional equipment; the all-stainless steel body is durable and corrosion-resistant, and the later maintenance difficulty and cost are far lower than similar products.
Enterprise Strength & Project Service Support

Qingzhou Foren Water Treatment Equipment Co., Ltd. is a professional manufacturer focusing on the R&D, production and customized matching of industrial water treatment equipment, rooted in Qingzhou, Shandong, China. We have been deeply engaged in the drinking water treatment equipment industry for many years, and we are well aware of the different raw water quality conditions and production standard requirements of water plants in different regions at home and abroad.
Unlike trading companies that only sell equipment, we have our own independent production workshops, complete processing and testing equipment, and a professional engineering and technical team. All our equipment is produced and processed by ourselves, and every set of finished equipment will pass strict water quality test and machine operation test before delivery to ensure that the equipment can operate stably after arriving at the customer's site.
We do not provide stereotyped standard equipment. According to the customer's local raw water test data, plant site conditions and production capacity requirements, we will tailor the most suitable water treatment system scheme. Our product coverage is wide, not only serving a large number of domestic water plant enterprises, but also exported to Southeast Asia, Africa, South America and other overseas markets, accumulating a large number of successful on-site installation and operation cases.
In terms of after-sales service, we provide one-stop full-process support including pre-sales scheme design, in-sales installation guidance and after-sales long-term technical support. For overseas customers, we can provide remote online debugging and technical guidance at any time, and support on-site door-to-door service according to project needs, ensuring that every customer's water production line can run efficiently and stably for a long time.
Hot Tags: large scale reverse osmosis system, China large scale reverse osmosis system manufacturers, suppliers, factory, commercial ro filter, full home reverse osmosis system, industrial reverse osmosis machine, reverse osmosis desalination, Reverse osmosis water treatment equipment, Single Stage RO Equipment