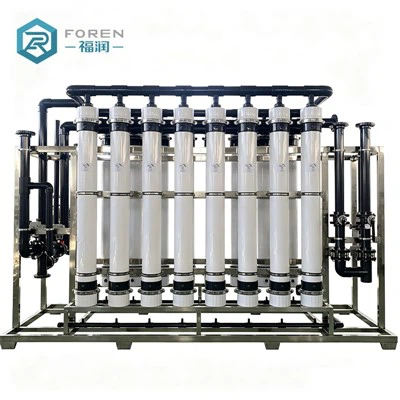

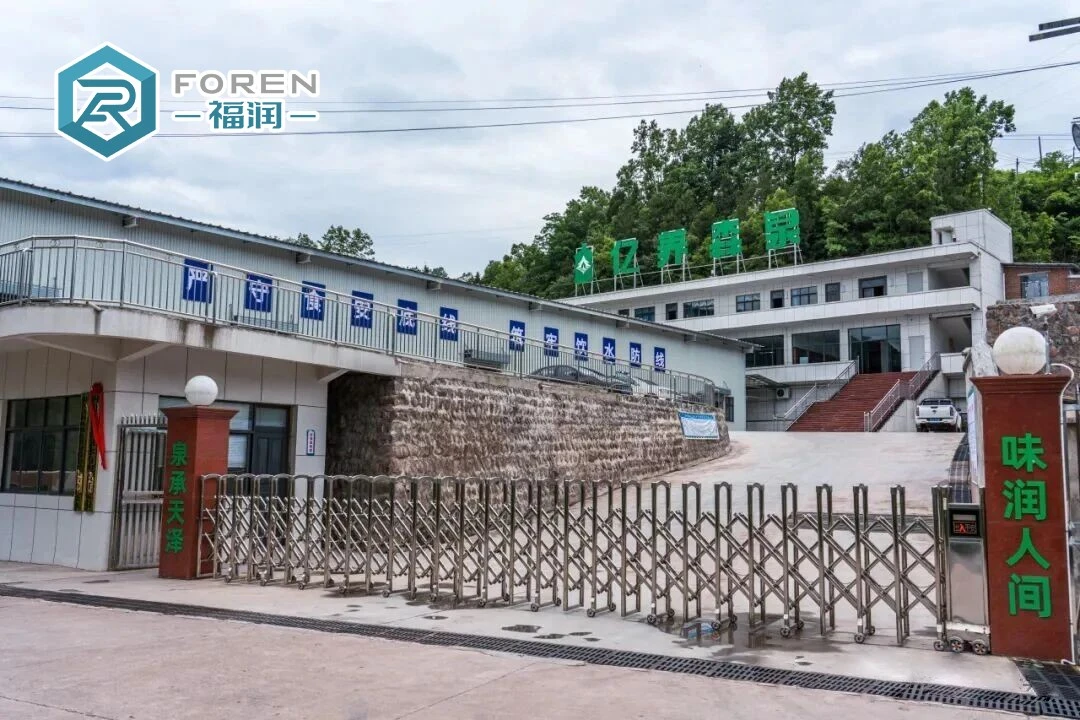
Qingzhou Foren Water Treatment Equipment Co., Ltd. specializes in customized water treatment processes and fully automated bottling line engineering for natural mountain spring and mineral water. The company provides nationwide one-stop services-including process design, equipment customization, on-site installation and commissioning, and full-line operational implementation-to water plants located at source sites. The Tongjiang Mountain Spring Water Plant project in Hongyan Village, Xinchang Town, Tongjiang County, Bazhong City, Sichuan (completed in July 2026), stands as a benchmark for the simultaneous implementation of dual production lines (bottled water and disposable large-format containers) utilizing nanofiltration technology to preserve minerals.
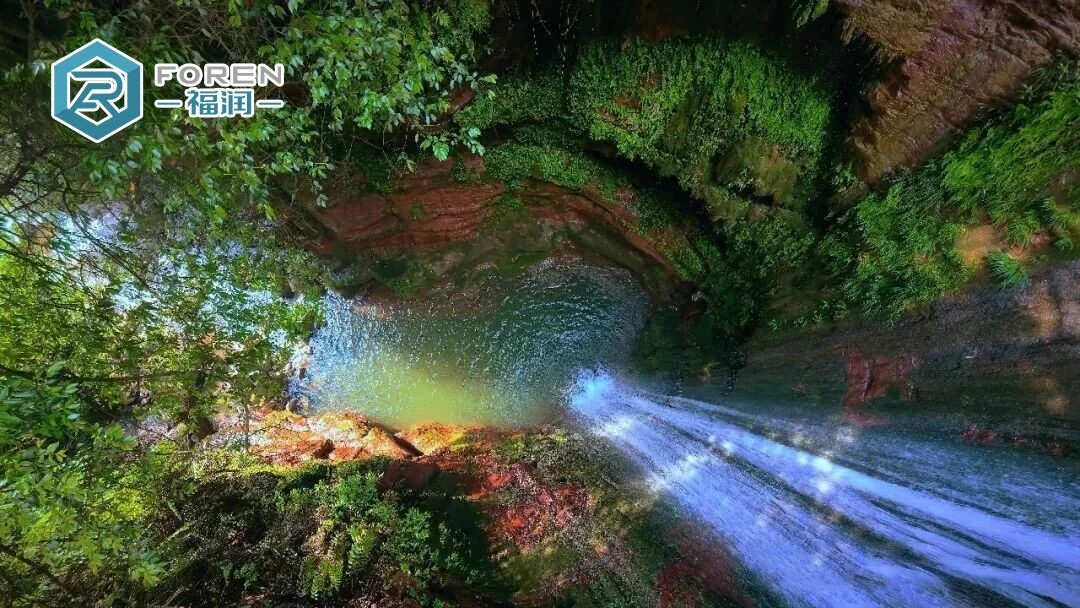
Located in the Longtangou water source zone of Hongyan Village, Xinchang Town, Tongjiang County, Bazhong City, Sichuan Province, the project draws upon self-gushing spring resources from the pristine forests of the Qinba Mountains. The source water is naturally rich in metasilicic acid, offering a crisp, sweet taste and moderate mineralization-qualities essential for premium natural mountain spring water products. Tailoring the solution to the raw water characteristics and brand positioning, Foren bypassed traditional reverse osmosis (pure water) processes in favor of a specialized system combining nanofiltration, instant UV sterilization, and long-lasting ozone bacteriostasis. The company delivered complete, fully automated production lines for both bottled water and disposable large-format containers-including blow-molding machines, 3-in-1 filling machines, coders, labelers, and packaging machines-enabling standardized, large-scale production.
Unlike standard purified water equipment on the market, this project addresses key challenges:
Achieving purification standards without demineralization and ensuring sterilization and freshness without leaving harmful residues. It thoroughly removes impurities, microorganisms, and pollutants while fully preserving the natural metasilicic acid minerals and original taste profile of the mountain spring water. This project serves as a model case study for the standardized construction of a premium metasilicic acid mountain spring water plant in the mountainous region of northeastern Sichuan.
Project Background and Implementation Details
• Implementation Year: 2026 (Official completion, opening, and full-scale production in July)
• Specific Location: Longtangou, Hongyan Village, Xinchang Town, Tongjiang County, Bazhong City, Sichuan Province
• Water Source Characteristics: Hongyan natural artesian spring in the Qinba Mountain region; naturally rich in metasilicic acid
• Production Scale: Simultaneous installation of two fully automated production lines-one for bottled water and one for disposable large-format containers (barrels)
A local team of returning entrepreneurs, leveraging high-quality local water resources, aims to create a flagship natural mountain spring water brand. Rejecting the homogenized path of ordinary purified water, they focus on product advantages such as "natural metasilicic acid content, pristine ecological origin, and high freshness." However, traditional purification processes could not balance water safety with mineral retention; therefore, they commissioned us to design a customized, end-to-end production solution to build a compliant, stable, and scalable high-end mountain spring water line.
Based on on-site water quality analysis and the brand's market requirements, the client's core objectives-which also presented the project's primary technical challenges-were clearly defined:
1. Strict control of water properties to preserve core selling points.
The use of reverse osmosis (RO) purification equipment was strictly prohibited; the process had to fully retain beneficial minerals-such as natural metasilicic acid and trace calcium and magnesium-and maintain the spring water's original, crisp, sweet taste. This avoids the common industry pitfall of "turning mountain spring water into purified water," thereby ensuring the brand's competitive differentiation.
2. Comprehensive purification to eliminate safety risks.
Open-air mountain springs are susceptible to seasonal sediment fluctuations, suspended matter from rainwater runoff, trace organic compounds, and microbial growth. Deep purification is essential to ensure the finished product meets all national standards for natural drinking spring water, allowing for consistent compliance in routine inspections and safe market distribution.
3. Dual-action bacteriostasis and preservation to stabilize taste.
Single sterilization methods have distinct limitations: ozone alone can produce by-products, while UV alone lacks long-term bacteriostatic capability. A combined sterilization system is required to achieve both immediate sterility and long-term preservation, ensuring the finished water maintains a stable taste, remains free of off-flavors, and prevents secondary bacterial growth throughout its shelf life.
4. Fully automated dual-production-line layout, adaptable to omnichannel sales.
To simultaneously serve the retail market (bottled water for supermarkets) and the single-use bulk container market (for households and commercial use), two independent, fully automated production lines are required. This setup achieves end-to-end automation-from bottle blowing to final packaging-thereby reducing labor costs and ensuring consistent product appearance and water quality standards.
5. Adaptability to raw water fluctuations in mountainous regions and low long-term maintenance requirements.
Water sources in mountainous areas experience minor quality fluctuations due to seasonal changes and rainfall; therefore, equipment must possess strong resistance to fouling and self-adjusting capabilities. Simple maintenance and low failure rates are essential for ensuring stable, high-volume production at mountain-based water plants.
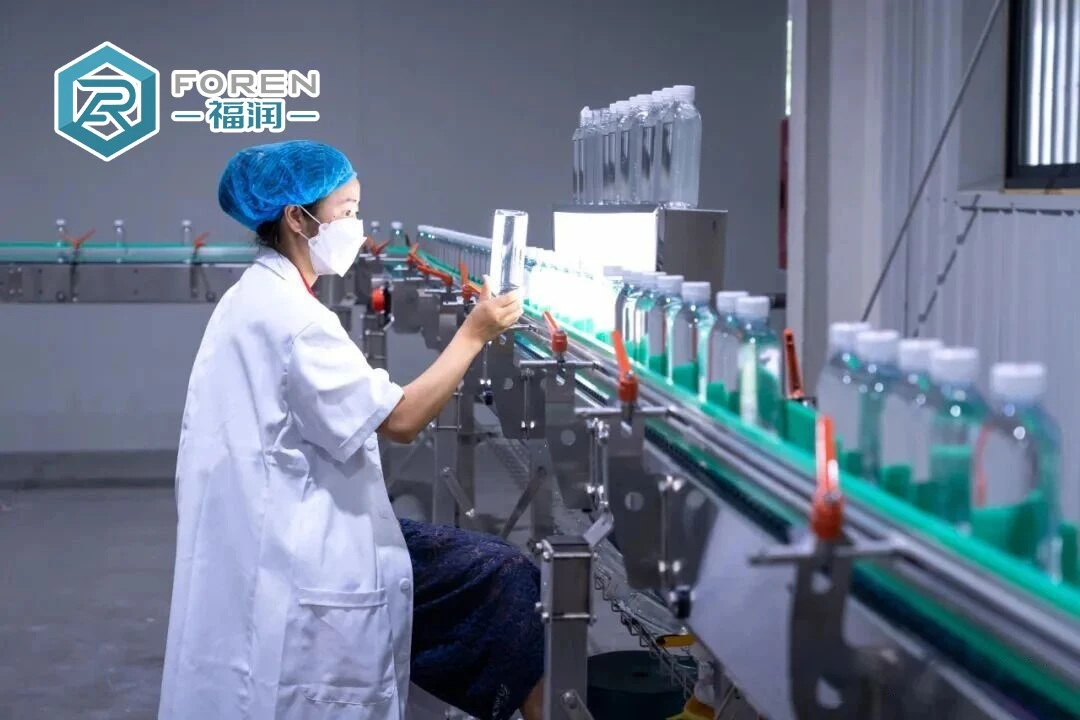
Our company has spent years developing mountain spring water plants in mountainous regions. We have observed that water plants in the mountainous areas of northeastern Sichuan commonly suffer from poor process adaptability-a key reason why many local spring water brands struggle to achieve premium positioning and standardization:
1. Reverse osmosis (RO) processes over-filter the water, stripping away the core value of mountain spring water.
Conventional RO systems offer extremely high filtration precision; while they remove impurities and bacteria, they also completely filter out beneficial components like metasilicic acid and trace elements. This effectively turns natural spring water into purified water, destroying the unique selling points that define premium spring water products.
2. Simple filtration processes lack precision, leading to highly unstable water quality.
Traditional combinations of sand filtration, activated carbon, and precision filtration can only remove large sediment particles; they fail to capture small-molecule organics, trace heavy metals, or colloidal impurities. During the rainy season, when turbidity rises, water quality frequently fails spot checks, making compliant, large-scale production impossible.
3. Single-method sterilization processes have flaws, resulting in inconsistent shelf life for the finished product.
Relying solely on ozone sterilization can generate by-products like bromate, compromising safety. Relying solely on UV sterilization provides only instantaneous disinfection without inhibiting subsequent bacterial growth in pipelines or the bottled water itself, leading to issues like deteriorated taste and excessive bacterial counts after storage.
4. Disjointed equipment and fragmented production lines result in low automation.
In many small water plants, purification and filling equipment are cobbled together without proper integration. This leads to process bottlenecks, excessive manual intervention, and low production capacity. The resulting product quality is inconsistent, making it impossible to support the brand's market-oriented and standardized operations.
Foren's On-Site, Customized Implementation Solution
To meet the specific requirements of Hongyan Village in Tongjiang, Bazhong, Sichuan-considering the actual operating conditions of the mountain spring source water, seasonal fluctuations, and the client's need for mass production across dual product lines-Qingzhou Foren Water Treatment Equipment Co., Ltd. rejected generic, standardized solutions. Instead, following on-site surveys and water quality analysis, the company developed an integrated implementation plan featuring a core "mineral-preserving" nanofiltration process, dual UV-ozone sterilization, and fully automated, turnkey dual-line delivery, all perfectly aligned with high-end mountain spring water production standards.
1. Core Water Treatment: Low-Pressure Selective Nanofiltration System for Precise Metasilicic Acid Retention
This project utilizes industrial-grade, low-pressure selective nanofiltration equipment. With membrane pore sizes positioned between ultrafiltration and reverse osmosis, the system employs a dual mechanism of physical sieving and charge adsorption to achieve "selective purification and differential mineral retention." The equipment efficiently removes sediment, suspended solids, colloids, macromolecular organics, heavy metals, scale-forming ions, and harmful impurities, while precisely retaining beneficial natural minerals such as metasilicic acid and trace amounts of calcium and magnesium. This effectively resolves the dilemma often faced with traditional equipment-where meeting purity standards results in mineral loss, yet preserving minerals fails to meet purity standards. The solution perfectly aligns with the product positioning of natural, metasilicic acid-rich mountain spring water, ensuring consistent mineral content, a crisp, sweet taste, and uniform quality across every production batch.
2. Dual-Stage Sterilization Process: A combined UV and ozone disinfection system ensures safety, sterility, and long-lasting freshness.
To address issues such as rapid microbial growth in mountain water sources and unstable shelf life for the finished product, the project incorporates a dual-disinfection system featuring a fully automatic UV sterilizer and an ozone generator. These complementary technologies provide comprehensive coverage with no weak points: UV sterilization handles instantaneous disinfection prior to filling, rapidly eliminating *E. coli*, pathogens, viruses, and other microorganisms without chemical additives or by-products, thereby guaranteeing absolute sterility before the water enters the filling stage. The ozone system ensures deep preservation, odor removal, and sustained bacteriostatic effects; it inhibits secondary contamination within pipelines and finished packaging, preserves the authentic taste of the mountain spring water, and significantly extends shelf life, fully complying with hygiene standards for the mass production of bottled and jugged drinking water.
3. Turnkey Delivery of Fully Automated Dual Production Lines: Integrated lines for both bottled water and single-use jugs.
Foren delivered two complete, independent, fully automated production lines for this project, meeting the brand's requirements across its entire product range. The process is fully automated and requires minimal manual intervention:
Fully Automated Bottled Mountain Spring Water Line: Includes a complete suite of equipment-automatic blow molding, bottle washing and disinfection, aseptic filling, precision capping, visual inspection, laser coding, automatic labeling, finished product conveying, and case packing. It supports the mass production of various bottle sizes, featuring seamless line integration, high filling precision, and consistent product quality.
Disposable bottled water production line: Features a complete aseptic filling line for single-use jugs. Unlike traditional systems using reusable containers, this approach eliminates cross-contamination at the source. It ensures high container cleanliness and an aseptic filling environment, making it ideal for high-end drinking water scenarios in homes, enterprises, and offices, while enriching the brand's product portfolio and expanding market reach.
The entire production line layout was optimized based on the specific site conditions of the mountain water plant. The equipment arrangement is compact and logical, facilitating easy operation and maintenance, ensuring low failure rates, and meeting the demands of long-term, full-capacity mass production.
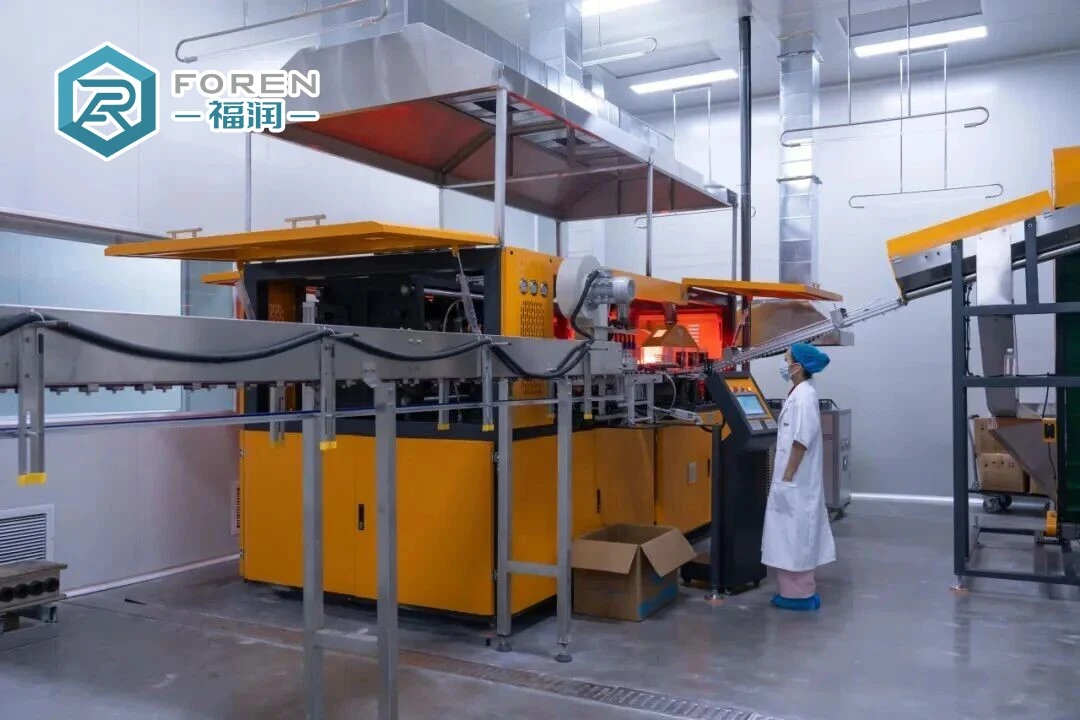
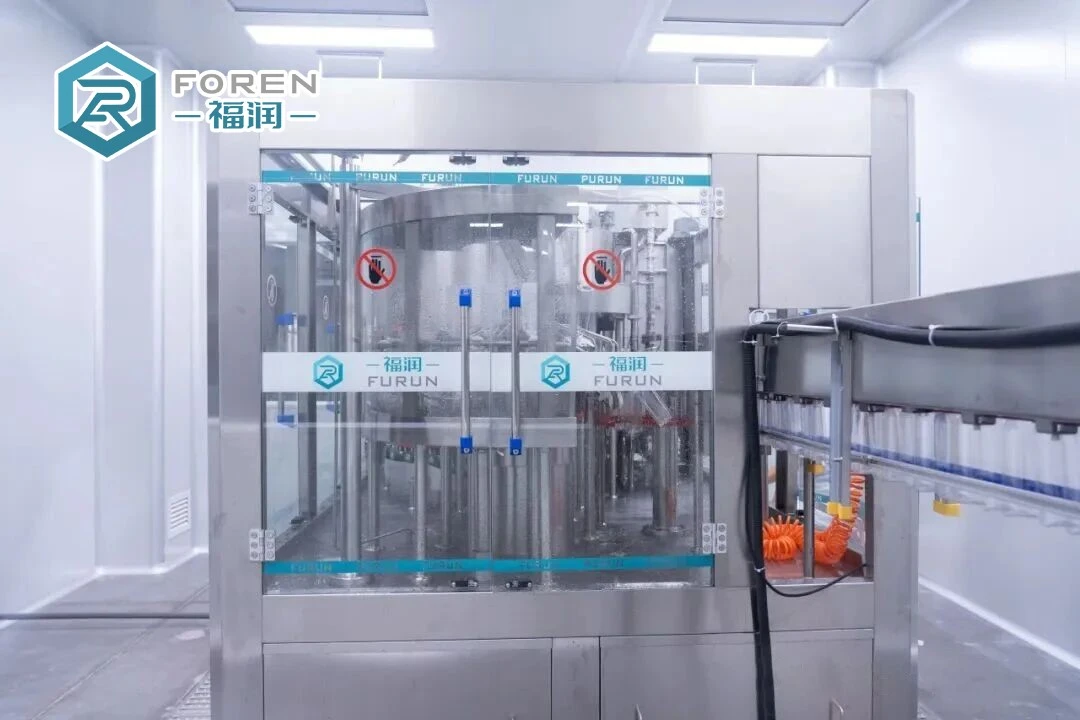
Since the project's full completion and commissioning in July 2026, the entire mountain spring water processing system has operated stably. All water quality and production capacity metrics meet standards, and the operational results significantly outperform traditional mountain water plant configurations:
1. Stable mineral content and preservation of key selling points:
Nanofiltration technology precisely retains the natural metasilicic acid found in the mountain spring water. The output features stable mineral levels and a crisp, sweet taste, distinguishing it from homogenized purified water on the market and creating a clear, high-end product advantage.
2. Compliant and controllable water quality suitable for routine inspections:
A combination of deep nanofiltration purification and dual-stage sterilization thoroughly resolves issues such as seasonal turbidity and excessive microbial levels common in mountain raw water. The output is clear, sterile, and consistent, fully complying with national standards for natural drinking spring water, making it safe for commercial distribution and regulatory testing.
3. Simultaneous mass production across dual lines to cover all market scenarios:
Bottled water caters to supermarkets, retail, and food service channels, while disposable large-format containers (barrels) serve households, enterprises, and commercial projects. This dual-product strategy significantly boosts brand market coverage and profitability.
4. High automation for cost reduction and efficiency gains:
The entire process-from bottle blowing to final packaging-is automated, drastically reducing labor requirements and operational errors. High production efficiency and simple maintenance make it ideal for the long-term, standardized, and brand-oriented operation of mountain water plants.
5. Robust equipment adaptability, resilience, and longevity:
Customized and optimized for the specific water quality fluctuations of the Bazhong mountain region, the equipment is fouling-resistant, easy to clean, and has a low failure rate. This effectively lowers long-term maintenance costs and extends the service life of the entire system.
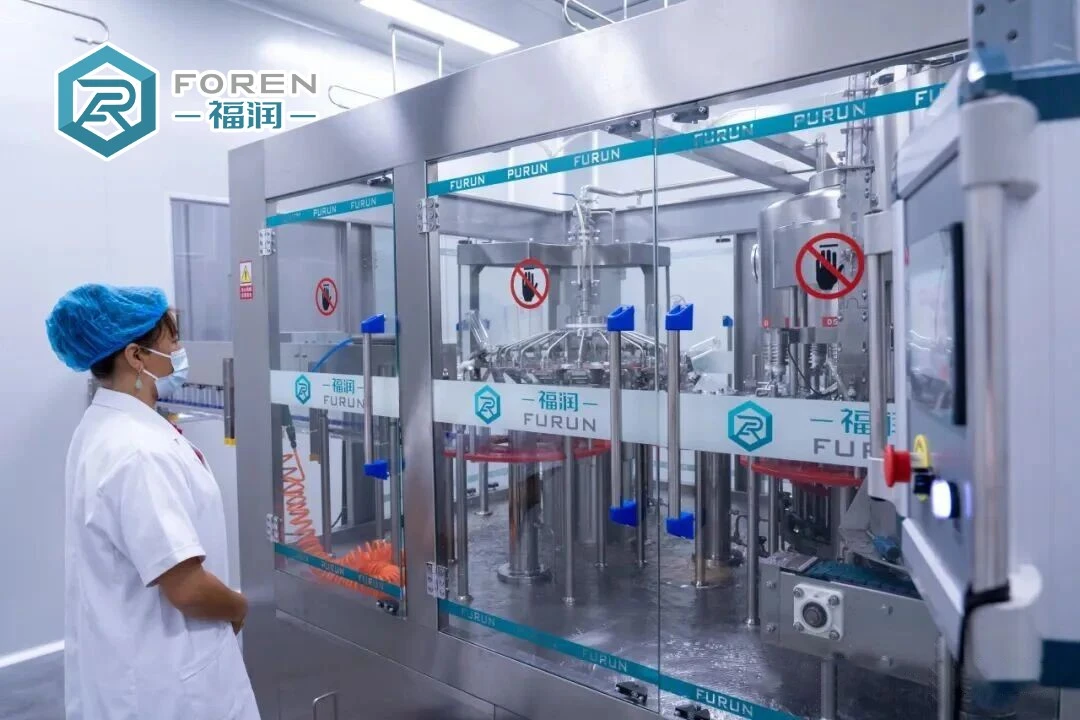
Core Industry Value and Project Summary
The Tongjiang Mountain Spring Water Project in Bazhong, Sichuan, serves as a benchmark for the successful implementation of mineral-preserving nanofiltration technology in a high-end mountain spring water plant in the mountainous region of northeastern Sichuan. The project demonstrates that for metasilicic acid-rich mountain spring sources, it is possible to meet water quality standards without sacrificing mineral content; through customized nanofiltration and dual-stage sterilization, the three core requirements-natural mineral properties, safety and regulatory compliance, and consistent taste-can be simultaneously achieved.
Qingzhou Foren Water Treatment Equipment Co., Ltd. specializes in customized, turnkey production line projects for high-end water plants utilizing natural mountain spring water, mineral water, or well water. We provide tailored water treatment processes and complete bottling/filling line solutions based on specific source water quality, client brand positioning, and production capacity requirements. We offer a comprehensive, one-stop service covering everything from site surveys, water quality testing, and process design to equipment manufacturing, on-site installation and commissioning, and post-launch after-sales support.
If you possess a high-quality water source-such as natural mountain spring or well water-and plan to launch your own drinking water brand, please contact Qingzhou Foren Water Treatment Equipment Co., Ltd. We provide complete solutions for fully automated bottling and disposable jug filling lines that ensure sterility and the retention of beneficial minerals (such as metasilicic acid). Our end-to-end services include on-site water quality testing, process customization, equipment selection, installation, production guidance, and lifelong after-sales maintenance, helping clients build high-end drinking water brands that are distinctive, compliant, and market-ready.
Related Links: Nanofiltration Mineral-Retaining Water Treatment Equipment | Fully Automated Integrated Bottling and Jug-Filling Production Line | Turnkey Plant Solutions for Mountain Spring and Mineral Water